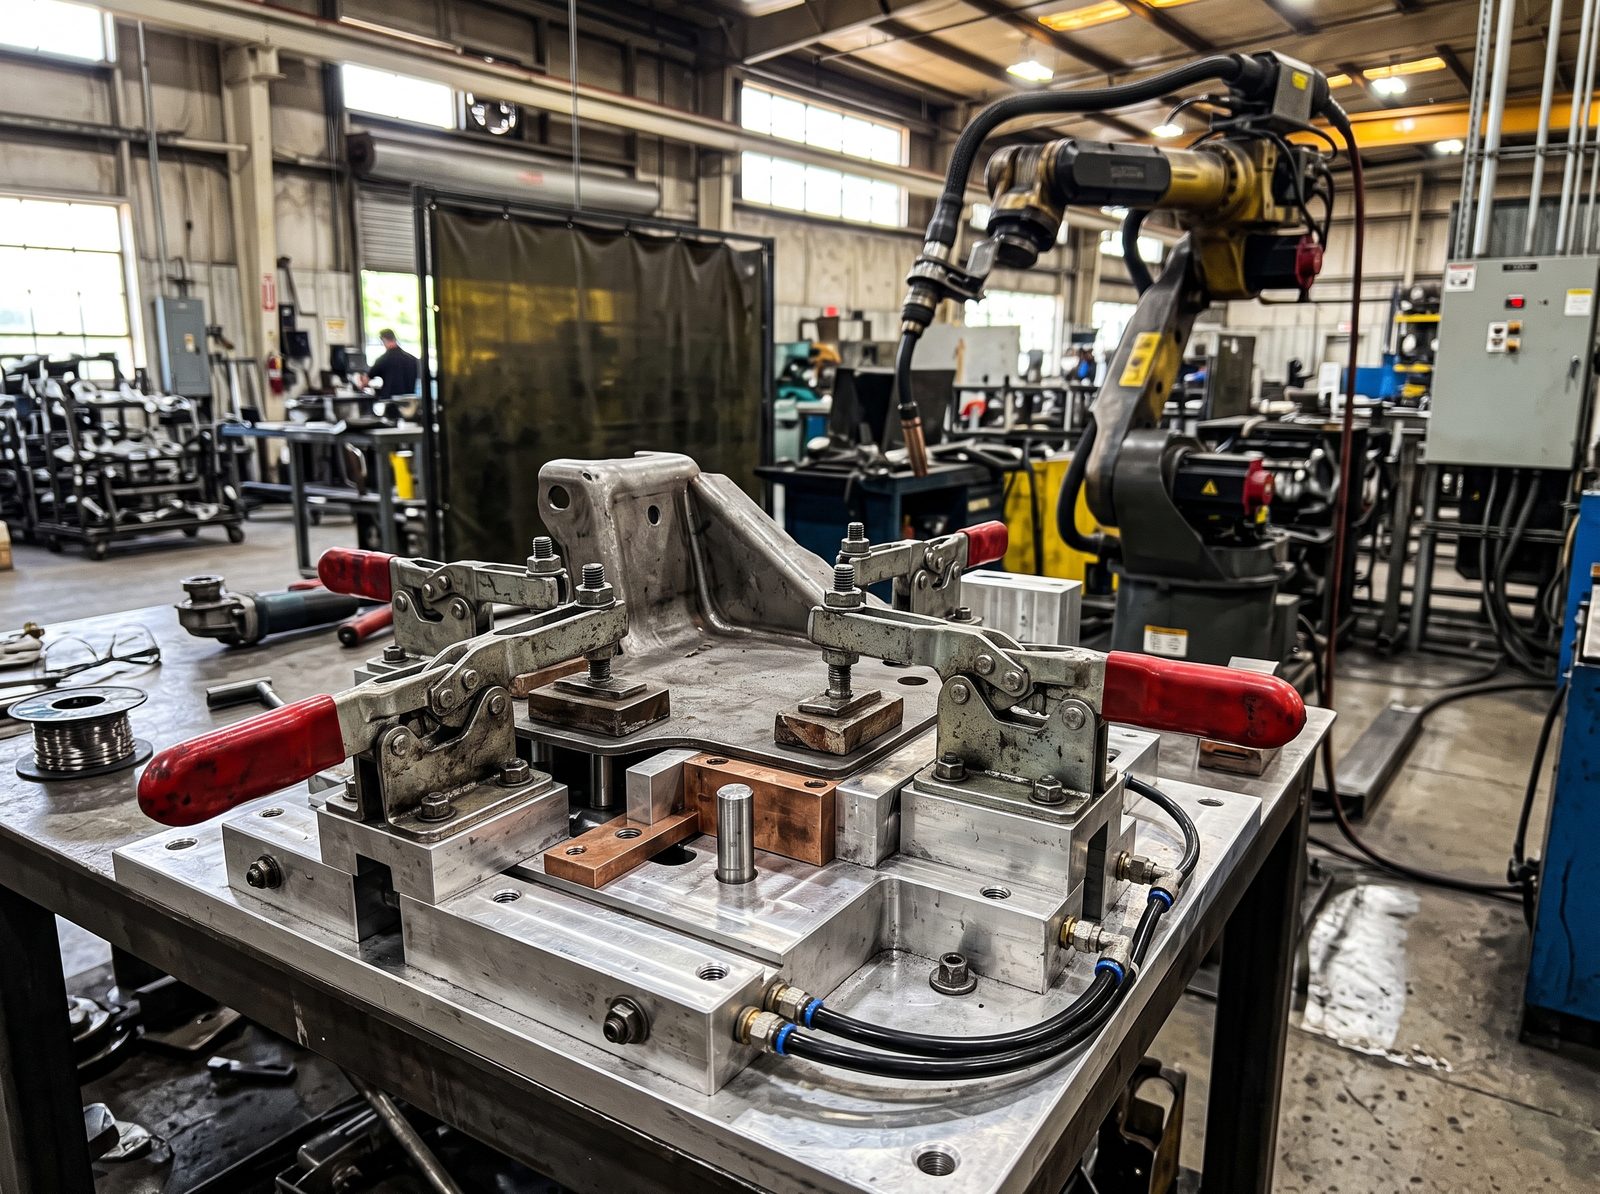
Jig & fixture for automotive part assembly
The problem
The old fixture did not locate the part repeatably, so weld positions drifted and parts had to be reworked. Scrap was highest at the start of a shift, before the machine had warmed up.
What we did
- Measured real parts and traced the drift back to specific clamping points before redesigning anything
- Designed five locating points with pneumatic clamps, shaped so the part cannot be loaded the wrong way round
- CNC machined with ±0.02 mm control at the datum features
- Every set inspected before shipping, with a dimensional report against the drawing
The result
- Weld positions now repeat on every part, cutting rework
- New operators are productive immediately because the part physically cannot be loaded incorrectly
- The dimensional report serves as evidence at incoming inspection
Delivered: fixture sets with spare wear parts · complete 3D and 2D drawings for every component · a dimensional inspection report per set