Packaging line control for a food plant
The problem
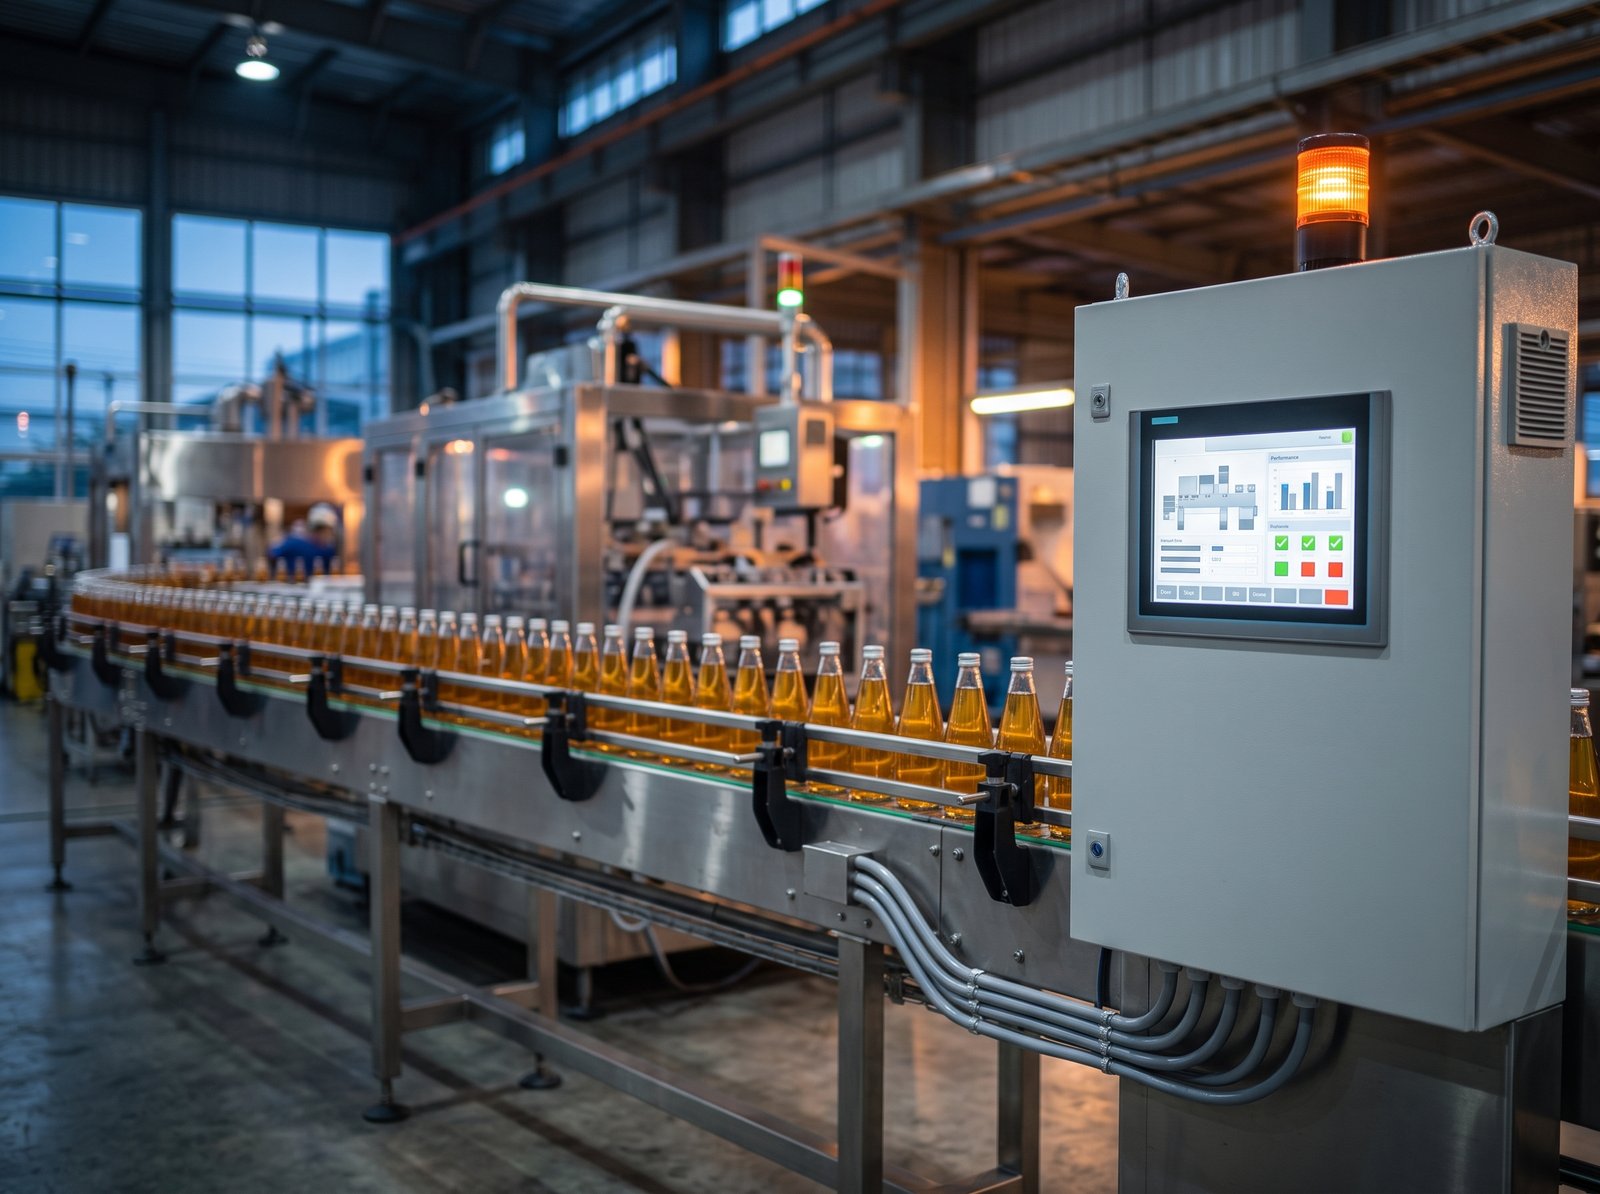
The line ran on relays and rotary timers. Every product changeover meant stopping the line and adjusting each timer by hand, costing about half a shift, and nothing recorded why the line had stopped.
What we did
- Captured the existing sequence as a state table and had the line leader review it line by line before any code was written
- Rewrote the PLC program from scratch, keeping safety (E-Stop, guard doors) separate from the production sequence
- Two HMI stations — a run screen, a recipe screen, and an alarm screen with history
- A central SCADA layer logging every second and publishing over Modbus TCP to the web monitor
The result
- Changeover is far faster than the half shift it used to take because recipes are called up from the HMI
- Every stop now has a reason — alarms are logged with a timestamp and the station that raised them
- Shift leaders check line status from a phone instead of walking to the machine
Delivered: PLC source and HMI project files · as-built I/O schedule and electrical drawings · FAT/SAT reports · a Thai-language operator manual